


Blog
Praced from Factory to O.R.: The Critical Importance of Prexa’s Validated Sterile Barrier Packaging

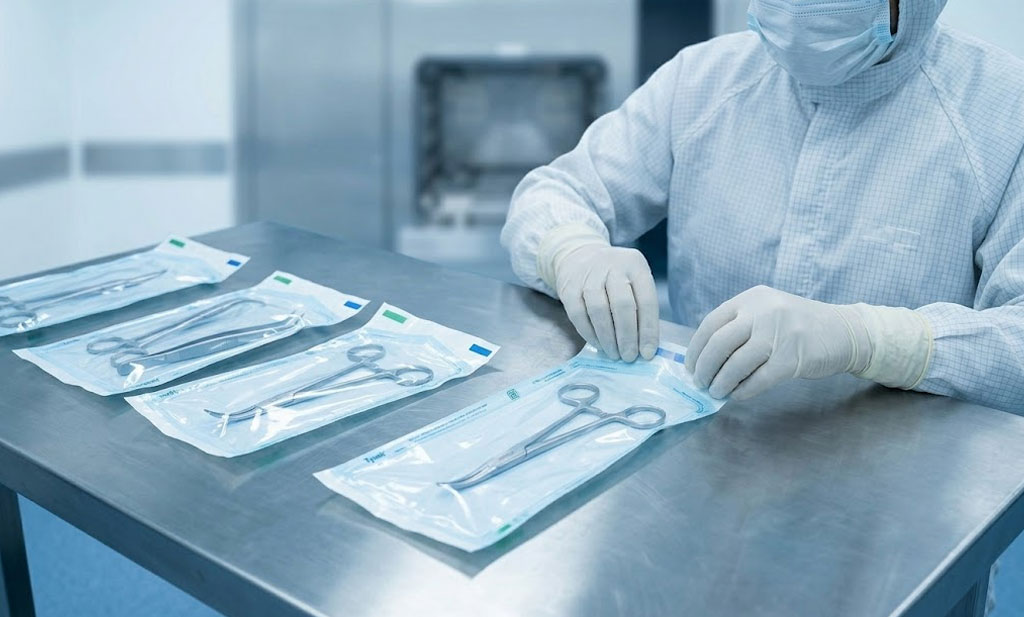
For a B2B healthcare importer, the product’s integrity must hold up throughout a complex global supply chain. This blog post details Prexa’s strict commitment to validation and sterility assurance from our production line to the operating room. We explain our validated cleanroom packaging process, where each premium single-use instrument (as seen being crafted in image_31.png) is sealed in custom-designed barrier pouches with clear indicator markings. This ensures protection against contamination during transit and storage. By partnering with Prexa, you can provide your clients with absolute confidence, knowing our packaging is a guarantee of safety.